SE CFETs Forge Better Connections
Posted: Thu Aug 20, 2026 7:01 am
Key Takeaways: 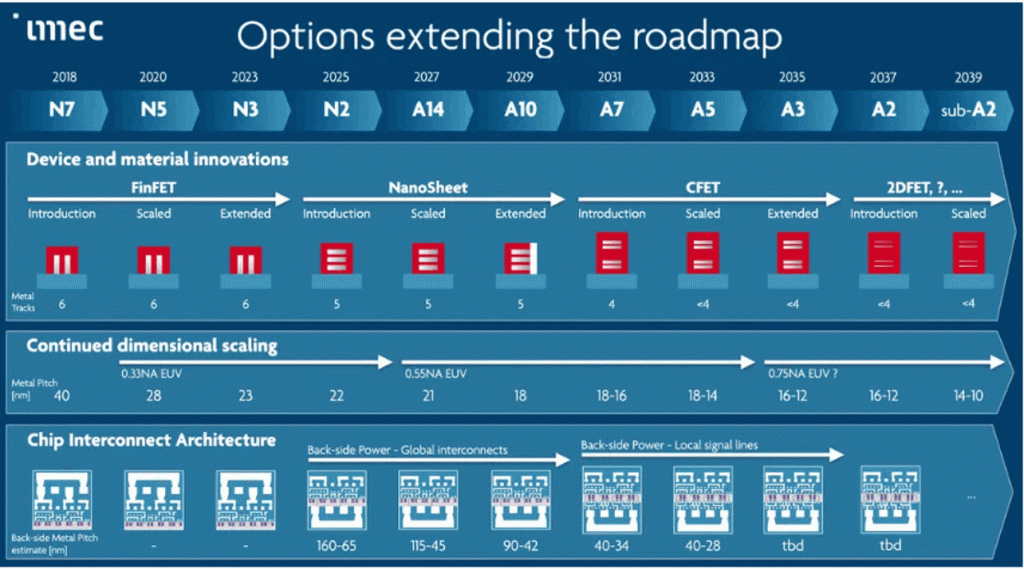 Fig.1: The roadmap shows the first CFET production at the A7 node around 2031 with critical dimension scaling below 18nm. Source: imec EUV patterning faces two problems as a direct result of the low total photon count per unit area (i.e., shot noise), which leads to variation in photon absorption, line-edge/width roughness (LER/LWR), and stochastic defects. At the same time, features are often taller to achieve higher aspect ratio etching, so pattern collapse is a concern. EUV underlayers can help. “EUV underlayers play an important role in improving lithographic performance by enhancing resist adhesion, reducing pattern collapse, and improving overall pattern fidelity,” said Brewer Science’s Guerrero. “Advanced underlayer materials can also help reduce line-edge and line-width roughness and, in some cases, lower required exposure dose by improving the chemical environment of the resist and mitigating stochastic defects.” Another technology that can address LER and LWR by etching away the rough edges is ion beam etching. IBE accelerates a highly collimated beam of ions at the resist pattern, and the beam tilt angle must be optimized for the process. EUV patterning and etching involve multi-layer optimization. “Silicon-containing hardmasks are commonly used during pattern transfer. After EUV exposure and development, the resist pattern is transferred into the silicon hardmask and subsequently into an underlying carbon layer,” Guerrero said. “Because the resist, silicon hardmask, and carbon layer exhibit different etch selectivity, the pattern transfer process can be precisely controlled through the choice of etch chemistries. This approach improves critical dimension control, pattern fidelity, and process integration flexibility.” Virtual fabrication’s role
Even before silicon starts, companies turn to virtualization to compare the many integration options. “The real challenge I’ve seen is people can think in planar technology quite well. Once you switch into the third dimension, it becomes much more difficult to keep track of what’s happening,” Ervin said. “With CFETs, now you’re adding another stack on top of a completely different stack, and it’s very complex. So that’s where you need computers because you’re trying to achieve atomistic-level accuracy. Any variation can have huge implications on yield.” Virtual fabrication and digital twins of processes dramatically reduce the number of actual wafers that need to be run in process development. “One important application of AI and machine learning is the creation of digital twins that simulate fab operations and process flows, reducing the need for costly and time-consuming physical experimentation,” said Guerrero. By comparing process windows across architectures, engineers can identify which design offers greater tolerance to manufacturing variations, fewer defects, and better overall performance. “The design engineer generally knows ‘this is exactly the device I want at the end of processing. But how do I make that?’ Ervin said. “That’s where the ingenuity and the art of making transistors comes in. Simulation is a good starting point because physics-based models are used. Engineers can compare putting nFET on top of pFET, or vice versa, and evaluate different integration schemes.” Simulation can also be used to optimize a technology once it is finalized. “Where we see a lot of interest now is in taking the initial nominal process case and injecting variation across it for each of the process steps to see what the outcome is going to be,” said Ervin. “We use machine learning to map the entire space around the nominal case, which provides a process window for each process step and the variation around it. You have an idea generally of what the equipment capabilities are in terms of deposition thickness or an epitaxial control etch depth and selectivity between materials, which you feed into the model right away.” Language models may be employed, as well. “AI gives you another engine to explore this space,” said Ervin. “We can use it to say, ‘I want to have no failures of these types in my technology. Can you find me something in the process integration flow to target those and make it manufacturable?’ The AI component can answer some of these questions. That really makes this an exciting field.” Conclusion
The CFET architecture is an exciting development for the semiconductor industry, increasing device density dramatically while promising 50% performance improvement and 70% less energy consumption. The early CFET publications out of TSMC, Samsung, Intel, and IBM are proving that although they all use the same basic processing tools of epitaxy, ALD, and etching, the process flows are slightly different. Companies are deciding between so-called split-gate processes with dielectric isolation and shared-gate with a depopulation approach that reduces parasitic effects. Although we think existing nanosheet transistors (i.e., non-stacked) are nearing the point where variation, warpage, and alignment issues are becoming untenable, CFET generation will need to do even better. By the time of production roll-out, around 2031, high-NA lithography will be more mature and simplify flows. Virtual fabrication is likely to play an even more pronounced role in pathfinding and yield improvement than it does today. References
The Sub-2nm Paradox
Reducing variation in manufacturing, monitoring behavior over time, and targeting specific workloads can have a big impact on power, performance, and area/cost. What’s Different About Next-Gen Transistors
Advanced etch holds key to nanosheet FETs; evolutionary path for future nodes. Big Changes In Architectures, Transistors, Materials
Who’s doing what in next-gen chips, and when they expect to do it. Backside Power Delivery Creates Fab Tool, Thermal Dissipation Barriers
Moving the power delivery network to the backside of a chip reduces congestion, but it introduces new challenges for fabs. The post CFETs Forge Better Connections appeared first on Semiconductor Engineering.
Source: https://semiengineering.com/cfets-forge ... nnections/
- Intel, Samsung, TSMC, and IBM are choosing different ways to connect nanosheet tiers, but all will use direct backside vias for backside power delivery.
- At the heart of CFETs are defect-free epitaxy, ALD dielectrics, workfunction-optimized metals, and perhaps layer transfer.
- Virtual simulation speeds pathfinding, integration, and yield-improvement efforts while saving the time and cost of actual silicon development.
- Wafer preparation
- STI formation
- Dummy gate formation
- Bottom S/D etch
- Bottom S/D growth
- S/D isolation formation
- Top S/D growth
- GAA formation
- Replacement metal gate
- MOL formation
- BEOL integration
- Nanosheet stack formation
- STI formation
- Dummy gate patterning
- N/P source/drain epitaxial integration
- ILD-0 planarization
- Nanosheet cut isolation
- Si nanosheet channel release
- Gate stack & multi-Vt integration
- MOL and BEOL integration
- Backside MOL and BEOL integration
Fig.1: The roadmap shows the first CFET production at the A7 node around 2031 with critical dimension scaling below 18nm. Source: imec EUV patterning faces two problems as a direct result of the low total photon count per unit area (i.e., shot noise), which leads to variation in photon absorption, line-edge/width roughness (LER/LWR), and stochastic defects. At the same time, features are often taller to achieve higher aspect ratio etching, so pattern collapse is a concern. EUV underlayers can help. “EUV underlayers play an important role in improving lithographic performance by enhancing resist adhesion, reducing pattern collapse, and improving overall pattern fidelity,” said Brewer Science’s Guerrero. “Advanced underlayer materials can also help reduce line-edge and line-width roughness and, in some cases, lower required exposure dose by improving the chemical environment of the resist and mitigating stochastic defects.” Another technology that can address LER and LWR by etching away the rough edges is ion beam etching. IBE accelerates a highly collimated beam of ions at the resist pattern, and the beam tilt angle must be optimized for the process. EUV patterning and etching involve multi-layer optimization. “Silicon-containing hardmasks are commonly used during pattern transfer. After EUV exposure and development, the resist pattern is transferred into the silicon hardmask and subsequently into an underlying carbon layer,” Guerrero said. “Because the resist, silicon hardmask, and carbon layer exhibit different etch selectivity, the pattern transfer process can be precisely controlled through the choice of etch chemistries. This approach improves critical dimension control, pattern fidelity, and process integration flexibility.” Virtual fabrication’s roleEven before silicon starts, companies turn to virtualization to compare the many integration options. “The real challenge I’ve seen is people can think in planar technology quite well. Once you switch into the third dimension, it becomes much more difficult to keep track of what’s happening,” Ervin said. “With CFETs, now you’re adding another stack on top of a completely different stack, and it’s very complex. So that’s where you need computers because you’re trying to achieve atomistic-level accuracy. Any variation can have huge implications on yield.” Virtual fabrication and digital twins of processes dramatically reduce the number of actual wafers that need to be run in process development. “One important application of AI and machine learning is the creation of digital twins that simulate fab operations and process flows, reducing the need for costly and time-consuming physical experimentation,” said Guerrero. By comparing process windows across architectures, engineers can identify which design offers greater tolerance to manufacturing variations, fewer defects, and better overall performance. “The design engineer generally knows ‘this is exactly the device I want at the end of processing. But how do I make that?’ Ervin said. “That’s where the ingenuity and the art of making transistors comes in. Simulation is a good starting point because physics-based models are used. Engineers can compare putting nFET on top of pFET, or vice versa, and evaluate different integration schemes.” Simulation can also be used to optimize a technology once it is finalized. “Where we see a lot of interest now is in taking the initial nominal process case and injecting variation across it for each of the process steps to see what the outcome is going to be,” said Ervin. “We use machine learning to map the entire space around the nominal case, which provides a process window for each process step and the variation around it. You have an idea generally of what the equipment capabilities are in terms of deposition thickness or an epitaxial control etch depth and selectivity between materials, which you feed into the model right away.” Language models may be employed, as well. “AI gives you another engine to explore this space,” said Ervin. “We can use it to say, ‘I want to have no failures of these types in my technology. Can you find me something in the process integration flow to target those and make it manufacturable?’ The AI component can answer some of these questions. That really makes this an exciting field.” Conclusion
The CFET architecture is an exciting development for the semiconductor industry, increasing device density dramatically while promising 50% performance improvement and 70% less energy consumption. The early CFET publications out of TSMC, Samsung, Intel, and IBM are proving that although they all use the same basic processing tools of epitaxy, ALD, and etching, the process flows are slightly different. Companies are deciding between so-called split-gate processes with dielectric isolation and shared-gate with a depopulation approach that reduces parasitic effects. Although we think existing nanosheet transistors (i.e., non-stacked) are nearing the point where variation, warpage, and alignment issues are becoming untenable, CFET generation will need to do even better. By the time of production roll-out, around 2031, high-NA lithography will be more mature and simplify flows. Virtual fabrication is likely to play an even more pronounced role in pathfinding and yield improvement than it does today. References
- Samuel K. Moore, “Future Transistor Stacking Plans Start to Diverge, IBM chooses a different path from Intel, Samsung, and TSMC,” IEEE Spectrum, June 25, 2026.
- D. Hwang et al., “First Demonstration of 3D Stacked Fets at Gate Pitch of 42nm Featuring Triple Stacked Nanosheet Channels for Advanced Logic Applications,” 2026 IEEE/JSAP Symposium on VLSI Technology and Circuits (VLSI Technology and Circuits), Honolulu, HI, USA, 2026, pp. 1-3, doi: 10.1109/VLSITechnologyandCir65830.2026.11577279.
- S. Liao et al., “CFET Demonstration for Future Logic and SRAM Technology,” 2026 IEEE/JSAP Symposium on VLSI Technology and Circuits (VLSI Technology and Circuits), Honolulu, HI, USA, 2026, pp. 1-3, doi: 10.1109/VLSITechnologyandCir65830.2026.11577430.
- J. A. Wiedemer et al., “Demonstration of CFET Inverters on Si (110) with 2X2 RibbonFETs at 45nm Gate Pitch with PowerVia and Direct Backside Contacts,” 2026 IEEE/JSAP Symposium on VLSI Technology and Circuits (VLSI Technology and Circuits), Honolulu, HI, USA, 2026, pp. 1-3, doi: 10.1109/VLSITechnologyandCir65830.2026.11577296.
- C. Zhang et al., “Area and Performance of Staggered-Channel Nanostack SRAM Bitcells,” 2026 IEEE/JSAP Symposium on VLSI Technology and Circuits (VLSI Technology and Circuits), Honolulu, HI, USA, 2026, pp. 1-3, doi: 10.1109/VLSITechnologyandCir65830.2026.11577402.
The Sub-2nm Paradox
Reducing variation in manufacturing, monitoring behavior over time, and targeting specific workloads can have a big impact on power, performance, and area/cost. What’s Different About Next-Gen Transistors
Advanced etch holds key to nanosheet FETs; evolutionary path for future nodes. Big Changes In Architectures, Transistors, Materials
Who’s doing what in next-gen chips, and when they expect to do it. Backside Power Delivery Creates Fab Tool, Thermal Dissipation Barriers
Moving the power delivery network to the backside of a chip reduces congestion, but it introduces new challenges for fabs. The post CFETs Forge Better Connections appeared first on Semiconductor Engineering.
Source: https://semiengineering.com/cfets-forge ... nnections/